

Europe's packaging regulation has applied since 12 August 2026, and the small strip of adhesive on a mailer box is no longer a minor detail - it is a compliance and labour question.
November 18, 2026 - Packaging buyers spent most of the past two years worrying about board: recycled content, weight, recyclability. The next round of pressure is arriving somewhere less obvious - the tape that holds the box shut, and the machine that applies it.
1. The regulatory clock
Regulation (EU) 2025/40 on packaging and packaging waste - PPWR - has been in force since 11 February 2025 and applies from 12 August 2026, replacing the 1994 Packaging and Packaging Waste Directive. According to the European Commission, the regulation sets a binding objective that all packaging placed on the EU market be recyclable in an economically viable way by 2030, alongside rules on recycled content, reuse formats and packaging minimisation.
2. Two consequences follow for anyone closing a carton.
First, mixed-material closures become a liability. A paper-based box sealed with a plastic film tape is, from a repulping standpoint, a fibre pack with a plastic contaminant stuck to it - the kind of input mills screen out or downgrade. That is why converters and brand owners have been shifting toward paper-based tear tapes and paper double-sided adhesive strips, which keep the pack inside a single material stream.
Second, packaging minimisation is now a design constraint, not a cost exercise. Analysts tracking the regulation note that PPWR caps empty space in e-commerce, grouped and transport packaging at 50%, enforceable from 2030 - a rule that pushes sellers toward right-sized boxes rather than one large carton plus void fill. Smaller, more varied box formats mean shorter runs and more changeovers on the packing line.
3. The demand backdrop is not shrinking
The compliance push lands on a market that is still growing. Smithers' study The Future of E-commerce Packaging to 2031 forecasts global e-commerce packaging to reach $105.2 billion by 2031, and the same research house values the corrugated packaging market at $240 billion in 2026, rising to $265 billion by 2031 in The Future of Corrugated Packaging to 2031.
Growth of that order does not remove labour from the process by itself. It does mean more boxes per shift, more SKUs, and more pressure on the step where tape is applied.
4. Where double-sided tape actually goes
In box plants and print finishing departments, double-sided adhesive is rarely applied to a full corrugated sheet. It is applied to small, flat components: mailer-box flaps, envelopes and courier bags, gift-box wraps, hang tags, card sleeves, and the peel-and-seal strips that let an end customer close a return without searching for a tape dispenser.
That is a hand-intensive operation in most small and mid-sized factories. An operator takes a blank, positions it by eye, lays a 5–15 mm strip of double-sided tape, presses it down, and stacks it. Repeat several thousand times per shift. Position drift, trapped air, liner handling and operator fatigue all show up as rework, and rework at this stage is expensive because the printing and die-cutting have already been paid for.
5. What changes when the step is automated
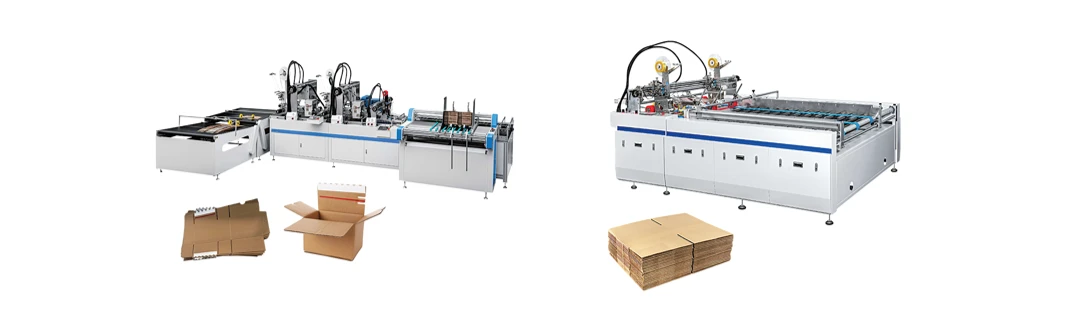
An automatic double-sided tape applicator replaces that cycle with a feeder, a tape head, a liner take-up and a stacker. In the machine class represented by Koten's WZ865A - the company's current automatic double-side taping model - the published envelope is 80–120 pieces per minute, for flat products from 40 × 40 mm to 200 × 200 mm and 0.2–5 mm thick, using tape 5–15 mm wide on rolls with a 76 mm core and up to 280 mm outer diameter, drawing 950 W at 220 V.
The economics are less about the headline speed than about three things:
- Consistency. A machine places the strip at the same distance from the edge on piece one and piece ten thousand, which is what brand owners auditing packaging quality actually check.
- Liner and scrap handling. Manual application leaves release-liner waste at the bench; a machine winds it up. In a factory where liner scraps end up in the corrugated waste stream, that alone changes the cleanliness of the baler.
- Labour redeployment. One operator can tend a machine rather than tape by hand, which matters in markets where packaging labour is the binding constraint.
6. What to check before buying a double-sided tape applicator machine
The specifications that decide whether a machine fits your work are narrower than the brochure suggests:
- Product size range. A machine rated to 200 × 200 mm cannot take a 300 mm mailer flap. Measure your largest and smallest blank first.
- Tape width range. Most e-commerce closures use 5–15 mm; gift-box and envelope work sometimes needs wider or dual strips. Confirm the head accepts the tape you actually buy.
- Tape roll format. Core diameter (commonly 76 mm) and maximum outer diameter determine how often the line stops for a new roll.
- Placement accuracy and adjustment. Ask how the strip position is set - mechanical stop, sensor, or servo - and how long a changeover takes between two SKUs.
- Substrate range. 0.2–5 mm covers paper, board and thin corrugated; film and foil behave differently and need a different pressure setting.
- Liner take-up and waste route. Where does the waste liner go, and can it be collected separately from production scrap?
- Power and footprint. A 950 W, 220 V single-phase unit on a 2000 × 780 mm frame fits a small finishing room; a three-phase line does not.
- Spare parts and service response. Tape heads wear. The cost of a stopped line for a week is far larger than the price difference between two machines.


